California Air Tools 20020AD vs a 10 HP Industrial Compressor: A Buyer's Side-by-Side
-
What I was actually comparing — and why it isn't a fair fight
-
Dimension 1: Noise — and why this turned out to be a compliance question
-
Dimension 2: What the extra horsepower actually buys you
-
Dimension 3: Infrastructure — the line item that never makes the quote
- Dimension 4: Where it's made, and whether you can get parts in year six
-
Dimension 5: Five-year cost of ownership
-
The search term that keeps showing up: air in a hydraulic cylinder
-
So which one should you buy?
-
What I'd verify before you sign
What I was actually comparing — and why it isn't a fair fight
I'm the office administrator for a 45-person fabrication and assembly shop. I manage facilities and MRO ordering — roughly $310,000 a year across 12 vendors. I report to operations and to finance, which means I get squeezed from both directions on every capital line.
Last fall our tired 60-gallon oil-lube compressor finally quit, and I got two quotes that were basically from different planets:
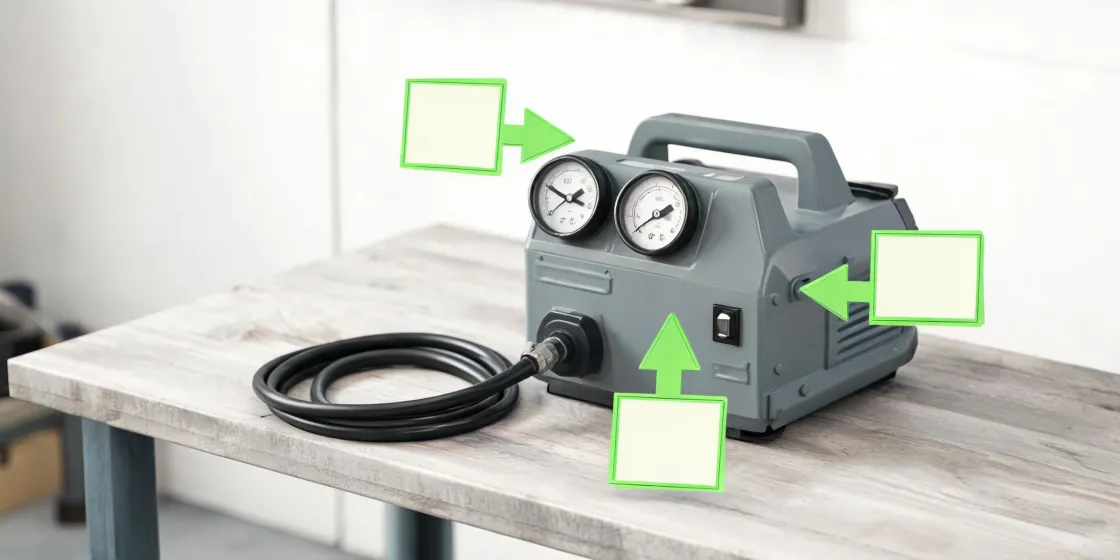
- Option A: an ultra-quiet, single-phase unit in the 10–20 gallon class — we ended up buying a California Air Tools 20020AD
- Option B: a 10 HP air compressor (two-stage reciprocating or small rotary screw), the kind a real production shop runs
I'm going to compare them across the five things that actually decided it for us: noise and placement, delivered air, electrical infrastructure, origin and parts support, and five-year cost of ownership. Plus a section on something that keeps landing in our maintenance search logs — how to get air out of a hydraulic cylinder — because it is almost never the problem people think it is.
One caveat up front: this is our situation, not a universal verdict. If you run a blast cabinet all day, close this tab and buy the 10 HP.
Dimension 1: Noise — and why this turned out to be a compliance question
Our old compressor sat in the corner of the main bay. Which meant it wasn't really equipment; it was a coworker. Around 85–90 dBA at three feet, and the guy running the press brake twenty feet away spent eight hours inside that field.
That matters because OSHA's general industry rule (29 CFR 1910.95, at osha.gov) sets a permissible exposure limit of 90 dBA over an 8-hour time-weighted average, with an action level at 85 dBA that triggers a hearing conservation program. Nobody in our shop ever wrote that down. But when I started looking at compressor noise as a documentation problem instead of a comfort problem, the calculus flipped.
The California Air Tools 20020AD publishes a sound rating around 70 dB. Full disclosure: that number is measured close to the unit, not at the operator's ear across your shop floor, so don't treat it as an exposure figure. What I can tell you is the practical difference — at that level, two people standing next to it can talk normally. At 88 dB, they can't.
Here's the part that surprised me. I expected "quiet" to be the first thing finance would cut. Instead it became the easiest line in the proposal to defend, because it eliminated the need for an exterior pad and a long electrical run — we'd been quoted about $2,800 for the pad work alone, plus conduit.
Then again, a 10 HP rotary screw in a factory sound enclosure can also land in the 65–75 dB range. It's just another $2,000–4,000 on top of an already bigger number.
Verdict: The ultra-quiet 10–20 gallon wins on freedom of placement. The 10 HP only competes on noise if you can put it in a mechanical room or pay for the enclosure.
Dimension 2: What the extra horsepower actually buys you
First, the thing that trips up almost every non-technical buyer: tank size is not capacity. The tank is a buffer. It absorbs surge — a nailer burst, an impact wrench hit — and it reduces how often the motor cycles. It does not change how much air the pump can sustain.
So when you're shopping a 10 gallon air compressor versus a 20-gallon unit in the same family, you're buying cycle frequency and surge headroom, not throughput. The 20020AD's bigger tank mostly means the motor starts fewer times per hour, which is easier on the motor and easier on everyone's ears.
Sustained delivery is where these two options separate hard:
- California Air Tools 20020AD: published output in roughly the 4–5 CFM range at 90 PSI, depending on which revision of the spec sheet you're reading. Verify the current figure with the distributor — they revise these.
- 10 HP industrial: typically mid-30s CFM at 100 PSI for a two-stage reciprocating unit, sometimes higher for rotary screw. That's roughly seven to eight times the air.
So the honest question isn't "which is better." It's "what's your real demand?" We counted ours: two framing nailers, one impact, a blow gun, and a plasma cutter that wants dry air. Realistic peak under 12 CFM, and never sustained. We would have been paying for 25 CFM we'd never use.
One more thing worth knowing: consumer-tier listings love to publish "peak HP" and a bare "SCFM" figure with no pressure attached. Compressor performance is standardized under ISO 1217, and CAGI publishes verified performance sheets. Ask for delivered CFM at 90 PSI. If a listing can't give you that number, that's your answer.
Dimension 3: Infrastructure — the line item that never makes the quote
A 10 HP air compressor is almost always three-phase, 208–230/460V. If your building doesn't have three-phase service, you're choosing between a rotary phase converter and a service upgrade. We were quoted $4,200–$9,000 for the upgrade depending on whether the utility had to pull new service to the building.
Even if you do have three-phase, budget for a dedicated disconnect and properly sized conductors. Per NEC Table 430.250, a 10 HP motor at 230V three-phase carries a full-load current around 28 amps — which means a 40-amp circuit and #8 copper at minimum, larger if the run is long.
In hindsight, I should have gotten the electrician's quote before I got the compressor quote. The compressor was never going to be the expensive part. But at the time, I was focused on the machine, because that's the thing with a spec sheet and a picture.
The 20020AD runs on single-phase 220V, which we already had from the old unit. If you don't have that circuit, add an electrician visit to both columns — it's just a much smaller one on this side.
Verdict: This dimension is where the 10 HP quietly loses. Not because it's bad, but because the true installed cost isn't the price on the listing.
Dimension 4: Where it's made, and whether you can get parts in year six
Where are California Air Tools made?
They're headquartered in Southern California, and they describe their compressors as designed and assembled in the U.S. using both domestic and imported components. That language varies by model, so check the specific product page rather than the brand homepage.
Here's why I care about the exact wording now, when I didn't in 2020. The FTC's Made in USA Labeling Rule holds unqualified "Made in USA" claims to an "all or virtually all" standard — meaning all significant parts and processing must be of U.S. origin. "Assembled in USA" is a different claim with a different bar. Details are at ftc.gov.
If a vendor's marketing uses "Made in USA" and their spec sheet says "assembled from domestic and imported components," ask which one appears on the invoice. Those two sentences have very different meanings, and only one of them is a legal claim.
For the 10 HP class, origin varies wildly — a lot of Chinese and Italian pump ends in that segment. But origin matters less to me than part number availability. Before you sign, ask for the parts breakdown PDF and spot-check three consumables: valve plate, gasket set, pressure switch. If any of those has no price and no lead time, you're buying a machine with an expiration date.
We once bought a machine where the manufacturer revised a control board, and a $40 part turned into a nine-week wait. The part cost was never the issue. The downtime was.
Dimension 5: Five-year cost of ownership
Purchase prices, based on published listings and distributor quotes I collected in January 2025 (verify current pricing — this segment moves):
- Ultra-quiet 10–20 gallon, single-phase: roughly $1,000–$1,500
- 10 HP two-stage reciprocating: roughly $3,000–$5,500, plus install
- 10 HP rotary screw: roughly $6,000–$11,000, plus install and usually a dryer
Power is more interesting than people assume. A 10 HP draws roughly 7.5 kW while running; our 2 HP unit draws about 1.5 kW. If the big unit runs 1,200 hours a year and ours runs 1,800 because it's slower, the annual energy cost isn't as lopsided as the nameplates suggest — specific power per CFM is broadly similar when both are sized correctly.
Where the 10 HP actually bleeds money is short-cycling. Big tank, small demand, and that motor starts and stops all day burning power to pressurize air nobody's using.
Then there's downtime, which is the number finance never models. For us, one three-hour line stoppage costs more than either compressor. The 10 HP wins that dimension when you genuinely need volume — and only then.
Verdict: For our demand profile, the ultra-quiet unit won on paper and in practice. The 10 HP only pencils out against continuous, high-volume demand.
The search term that keeps showing up: air in a hydraulic cylinder
I want to address this one directly, because I've watched people try to solve it by buying a bigger compressor, and that's the MRO equivalent of buying a bigger hammer.
If your hydraulic press, lift, or cylinder feels spongy, drifts, or runs hot, trapped air is a fluid-side problem. It does not get fixed from the air side. The actual process, roughly, is: check reservoir level and make sure the pump isn't pulling air through a loose suction line; cycle the cylinder slowly through full extension and retraction several times to push air back to the reservoir; with the rod slightly extended, open the bleeder screw at the high point of the cylinder and let fluid weep until it runs clean and bubble-free; close it, top off the reservoir, and repeat until response is firm. Many cylinders have no bleeder screw — in that case you crack the fitting at the highest port.
Do not use a shop air compressor to purge a hydraulic cylinder. High-pressure hydraulic fluid can inject through skin at pinhole size, and those injuries are surgical emergencies — NIOSH and OSHA both publish warnings on this. Depressurize and cycle the system before you open anything.
I'm not a hydraulic technician, so I can't walk you through your specific machine. Our maintenance lead does the bleeding; my job is making sure fluid and seals are on the shelf before we run out. If your equipment is under a service contract, pay the OEM and keep the paperwork.
The one legitimate overlap between these two worlds: air-over-hydraulic pumps. Those use regulated shop air — usually 80–100 PSI — to drive a hydraulic circuit. If that's your setup, then yes, your air supply matters, and so does dryness. A filter/separator on that line runs $60–$200 and prevents a whole category of problems.
So which one should you buy?
Go with the ultra-quiet 10–20 gallon (California Air Tools 20020AD class) if: your real peak demand sits under about 12 CFM; your tools are nailers, impacts, blow guns, and light spraying; noise and placement matter; you don't have three-phase; and you want to be all-in for $1,000–$1,800 including a circuit.
Go with the 10 HP industrial if: you need sustained demand above roughly 20 CFM; you're running a blast cabinet, multiple DA sanders, tire service, or production painting; you already have three-phase; and you can put it in a room where nobody has to stand next to it.
Two things not to do. Don't buy a 10 HP because it's "future-proof" — idle capacity still costs you oil changes, filters, and electricity. And don't pick your tank size on price alone, because in this class the tank is a buffer, not a capacity rating.
What I'd verify before you sign
Delivered CFM at 90 PSI from the current spec sheet (ISO 1217 / CAGI methodology), the electrical quote in writing, three part numbers with prices and lead times, and the exact origin language on the invoice — not the website. Noise data is worth checking against OSHA 1910.95 at osha.gov, and origin claims against the FTC's Made in USA standard at ftc.gov. Prices above are from listings and quotes collected January 2025 and are for general reference only; verify current rates before you build a budget around them.
Bottom line: I bought the quiet one, and I'd buy it again. But that's because I counted our CFM first. Do that part before anything else.
Helena Duarte
Helena Duarte is an independent pipe, valve, and pump applications analyst covering fittings, ball valves, gate valves, check valves, butterfly valves, flanges, hose clamps, centrifugal pumps, sump pumps, and submersible pumps. She uses ISO 5208 pressure-testing concepts and ISO 9906 pump acceptance methods while comparing pressure class, seat leakage, Cv, head, flow, efficiency, solids passage, seal materials, and installation orientation. Her guides help specifiers and maintenance teams match fluid-handling components to service conditions and acceptance criteria.